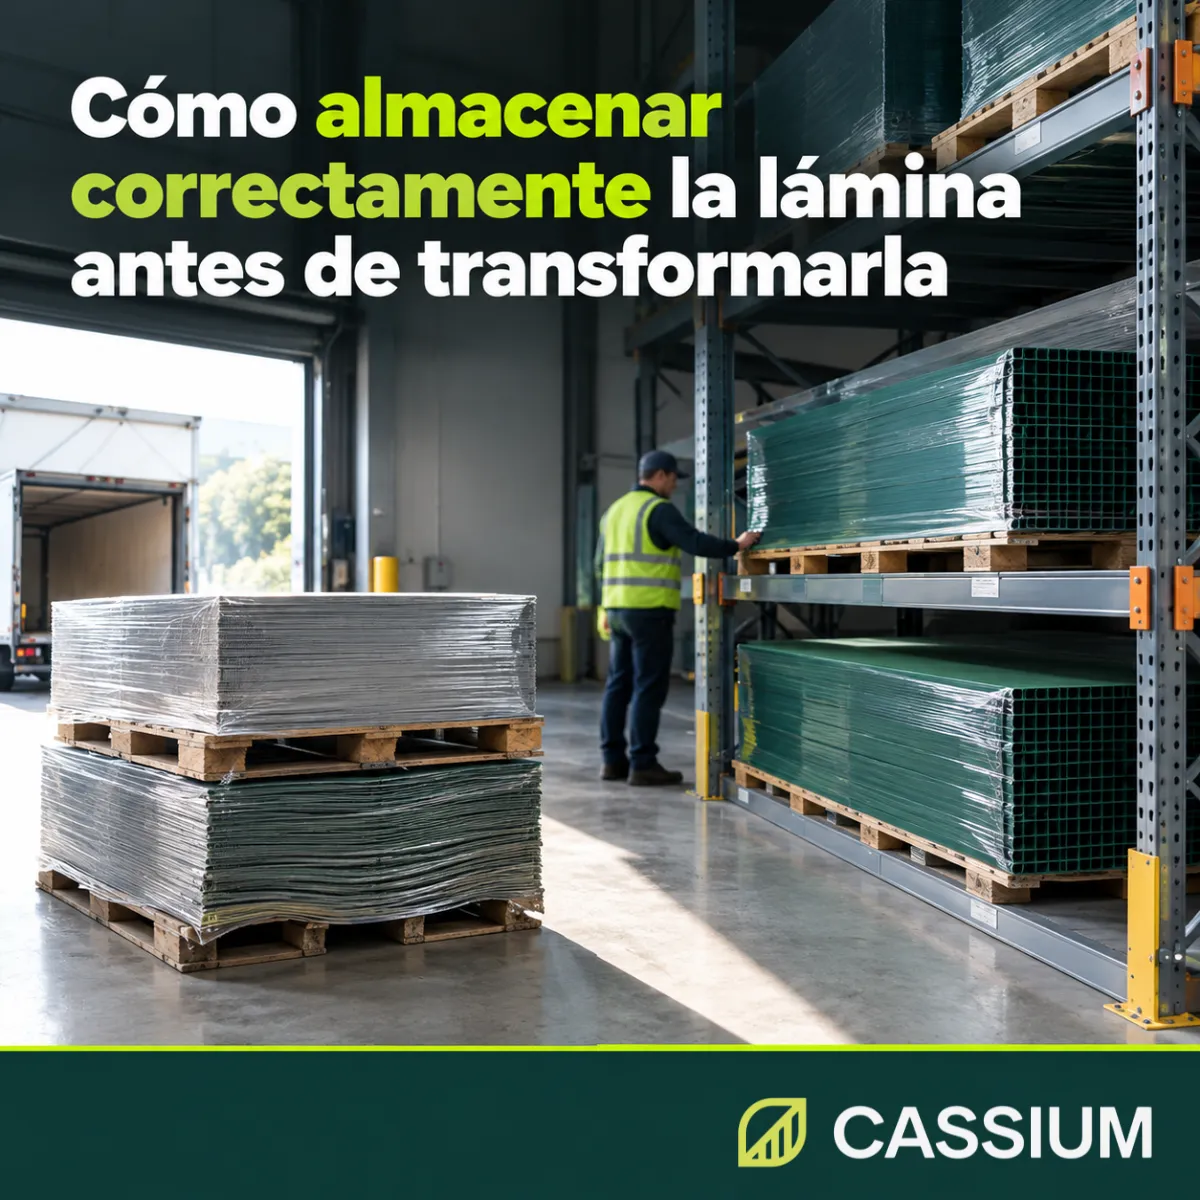
Store sheet lying flat on a base the size of the sheet, under a roof, away from sun and heat, with nothing on top and with rotation by batch. If you are going to print it, use it while the corona treatment is still effective.
What happens to a flat sheet after weeks of poor support
Sheet comes off the extruder flat and is checked for flatness before it goes onto the pallet. From that moment on, its flatness depends on how your warehouse supports it. Polypropylene is a thermoplastic, and it responds to two things every warehouse has in abundance: time and load.
Creep: the sheet's own weight bends the edges
Under a constant load, polypropylene deforms little by little, a phenomenon materials engineering calls creep. A 1.22 by 2.44 meter sheet resting on a smaller base leaves overhanging edges that carry their own weight day and night, and within a few weeks they stay bent toward the floor. A pallet with spaced or broken boards leaves unsupported zones where the stack sags slightly, and the sheets at the bottom take on that shape.
The practical rule is simple: the base must be flat, complete and at least as large as the sheet. If your pallets are smaller than the sheet, place a rigid board the size of the sheet on top before stacking.
Internal stresses that heat releases unevenly
Every extruded sheet retains some internal stress from cooling, and a well-tuned line keeps it low and symmetrical. If one side of the stack gets more heat than the other, for example the side facing a sunlit wall or a hot machine, each face relaxes at its own pace and the sheet ends up with a bow that often becomes visible only when you cut it into small parts.
Heat, sun and cold: the damage that shows up after receiving
Sheet that arrived in good condition can change in your warehouse without anyone touching it, because of temperature, sunlight or sudden shifts between cold and warm areas.
Temperature: metal roofs, docks and heat sources
In a plant in northern Mexico during the summer, the top level of a rack under a metal roof can be much hotter than the floor. The same happens next to ovens, compressors and extruders, or on the dock where the afternoon sun hits. The higher the temperature, the faster creep progresses and the more easily internal stresses are released. Store sheet in the coolest and most stable area of your warehouse.
UV radiation: photodegradation starts before converting
Standard sheet is made without a UV additive, so direct sunlight starts degrading its surface within the first days of exposure. A pallet that spends weeks in the yard, or next to an open dock door that gets sun every afternoon, reaches the die cutter with its exposed face duller and more brittle than the rest of the stack. The clear stretch film that wraps the pallet lets much of that radiation through, so it does not work as sun protection either.
Cold and condensation: sheet that comes in from the yard in winter
Polypropylene loses toughness in the cold. Sheet that spent a winter night in a trailer and goes straight to the die cutter cracks more easily at cuts and scores. If it also moves abruptly into a warm, humid area, it becomes covered in condensation that interferes with printing and with any adhesive. Let the sheet reach the temperature of the converting area, still wrapped, before you open the pallet.
Water, dust and static: what stays in the flutes and on the face
Polypropylene absorbs practically no water, so ambient humidity leaves its stiffness intact. That leaves two open fronts: water that gets into the flutes and whatever sticks to the surface.
Water in the flutes: it gets in easily and comes out slowly
The flutes of the sheet are open at both ends of each sheet. A pallet exposed to rain, a roof leak or floor washing water holds that water inside the flutes for days. When the sheet is cut or die cut, the water runs onto the table, stains the print and travels inside the finished part all the way to your customer's packaging. Store pallets off the floor and away from downspouts and wash areas.
Dust and static charge on the face to be printed
The polypropylene surface builds up static charge through friction, and that charge attracts dust from the air. A dusty sheet prints with voids, holds a label poorly and carries particles into a part that goes into a clean area. Keep the wrapping on until you use the material, and cover the pallet again if you only took part of it.
Stacking that marks, scratches and crushes the sheet below
Stacking pallets frees up floor space, and the sheet pays for that savings, as the weight of whatever goes on top shows.
Half a ton on the top sheet of the pallet below
With our standard size of 1.22 by 2.44 meters, a pallet of 275 sheets of four millimeters and 600 grams per square meter adds up to about 490 kilos of sheet, and one of 160 sheets of six millimeters and 1,300 grams comes to around 620 kilos, not counting the pallet. When you place one on top of another, that weight rests on the top sheets of the pallet below through the boards of the base, and the boards leave their mark: strips of crushed ribs that show on the face and lose strength. If you need to use the height, use racks where each pallet rests on its own level, and never put product or other materials on top of the sheet.
Forklifts, dragging and handling loose sheets
The forklift tines go only into the openings of the pallet; a tine that brushes the stack crushes the edges of several sheets at once. When you pick up loose sheets, lift them instead of dragging them across the one below, because friction scratches both faces and that scratch shows up later in a print or on a visible part. A 2.44 meter sheet lifted from one end bends halfway along its length, so it is best moved by two people.
Corona treatment and rotation by batch: sheet for printing has a use-by date
Stored properly, sheet keeps its mechanical properties for a long time. Sheet with corona treatment for printing is the exception, and the reason lies in its surface.
Why corona treatment loses effect in storage
Corona treatment is an electrical discharge that modifies the polypropylene surface so the ink can anchor. That effect fades over time, and warehouse heat speeds up the loss. Sheet that printed well the month it arrived can lose its ink months later, even if it looks identical. That is why treated sheet is bought at the pace of your printing jobs and checked before a long run with dyne pens or surface tension test inks, against the level your ink or your printer requires.
First in, first out by batch number
The batch label on each pallet lets you trace its run if something goes wrong. Keep it until the last sheet is used, arrange pallets so the oldest goes out first and avoid mixing sheets from different batches in the same parts order, especially when color or print has to match. If a part fails, the batch tells you whether the problem came from the sheet or from the warehouse.
The five minutes that keep you from converting damaged sheet
Before you open a pallet for production, lay one sheet on a flat table and check that all four corners touch the surface. Confirm that the sheet has reached the temperature of the work area, that the flutes are dry, that the face to be printed is clean and free of scratches, and that the corona treatment passes the test if the job carries ink. Write the batch number on the work order and convert with the confidence that the sheet is in the same condition it left the plant.
At Cassium we verify gauge, grammage, flatness and color for every batch before releasing it, and we record every run under our ISO 9001:2015 quality management system at our plant in Santa Catarina, Nuevo León. Since we deliver in 48 to 72 hours in northeastern Mexico, you can order sheet at the pace of your production instead of filling your warehouse with months of inventory. If you have questions about how to store a specific variant, such as corona-treated or ESD sheet, we will guide you before you place your order.
If sheet that arrived flat ended up bowed, marked or unable to hold ink, the damage most likely happened in your warehouse. At Cassium we make sheet from 2 to 6 mm, release it with verified flatness and grammage and deliver it at the pace of your production. Find your starting gauge, grammage and variant with our Recommender at https://cassium.com.mx/en